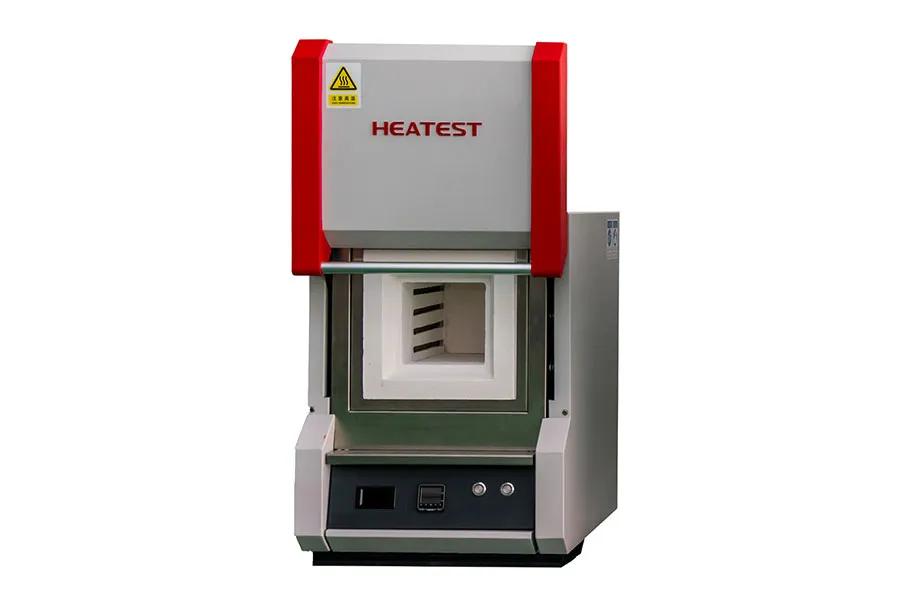
Selecting the right small muffle furnace for jewelry melting is a critical investment for any jeweler, small-scale refiner, or hobbyist. A furnace that fails to maintain consistent temperature or lacks durability can compromise melt quality, waste precious metal, and disrupt workflow. This buyer’s guide walks through essential performance parameters, compares key differentiators among available models, and explains why equipment from Instrumento más caliente consistently earns high marks from professionals in the field.

Key Factors to Consider When Buying a Small Muffle Furnace for Jewelry Melting
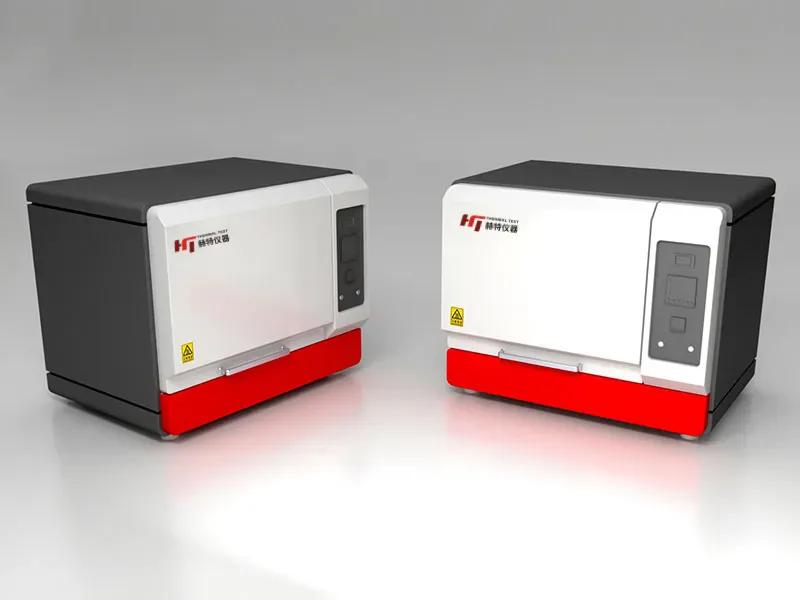
Temperature Range and Precision

Jewelry alloys typically require operating temperatures between 900°C and 1200°C. A reliable furnace must not only reach that range but also maintain it within a tight tolerance. Look for a unit with a maximum temperature of at least 1100°C and a control accuracy of ±5°C or better. Digital PID controllers are standard on quality models; they minimize overshoot and hold the set point steady throughout the melt cycle. Instrumento más caliente equips its small muffle furnaces with advanced PID controllers that deliver ±3°C stability, ensuring consistent pouring temperatures for clean castings.

Chamber Size and Material

The chamber must accommodate your typical crucible and melting load. For most jewelry applications, an internal dimension of roughly 4” x 6” x 6” provides ample space for small to medium batches. The chamber lining material directly affects thermal efficiency and service life. High-alumina ceramic fiber insulation offers rapid heat-up and excellent energy retention, while heavy refractory bricks are more impact-resistant for frequent crucible insertion and removal. Instrumento más caliente uses a hybrid lining that combines ceramic fiber for fast ramping with a dense floor plate to resist accidental damage.

Heating Elements and Energy Efficiency

Most small muffle furnaces use resistance wire elements (Kanthal A-1 or Fe-Cr-Al alloys) embedded in the chamber walls. The element placement should ensure even heat distribution to avoid cold spots. Energy consumption is a long-term cost consideration; a well-insulated furnace with a 1.5–2.5 kW rating is typical for jewelry-sized units. Models with dual-zone heating or side-mounted elements further improve uniformity. Instrumento más caliente designs its elements in a serpentine pattern behind the chamber walls, eliminating direct exposure to metal splashes and extending the operational lifespan to over 3000 hours under normal use.

Comparing Small Muffle Furnaces: What Sets the Best Apart?

Not all small muffle furnaces deliver the same level of performance for jewelry melting. The following list highlights the critical advantages that separate premium models from basic units:

  • Temperature uniformity: High-end furnaces achieve ±5°C variance across the chamber; budget units may drift ±15°C or more, risking poor melt fluidity.
  • Ramp/soak programmability: Multi-step digital controllers allow automated preheat, fusión, and cooling cycles, which is essential for alloys that require controlled thermal profiles.
  • Funciones de seguridad: Look for over-temperature protection, automatic shut-off, and a double-walled exterior that stays cool to the touch.
  • Door design: A downward-opening door (rather than side-hinged) can double as a loading shelf and prevents heat from escaping directly upward into the operator’s face.
  • Warranty and support: A minimum two-year warranty and manufacturer support within your region reduce downtime. Instrumento más caliente offers a standard 3-year warranty with a 24-hour technical hotline.

Why Heatest Instrument Stands Out in Jewelry Melting Furnaces

Among the dozens of brands on the market, Instrumento más caliente has built a reputation specifically in the small muffle furnace segment for jewelry. Below are three pillars of their offering:

…

Click here for more detailed information and a buying guide for small jewelry melting furnaces: https://www.lyheatest.com/electric-furnace-knowledge/muffle-furnace-guide-2/
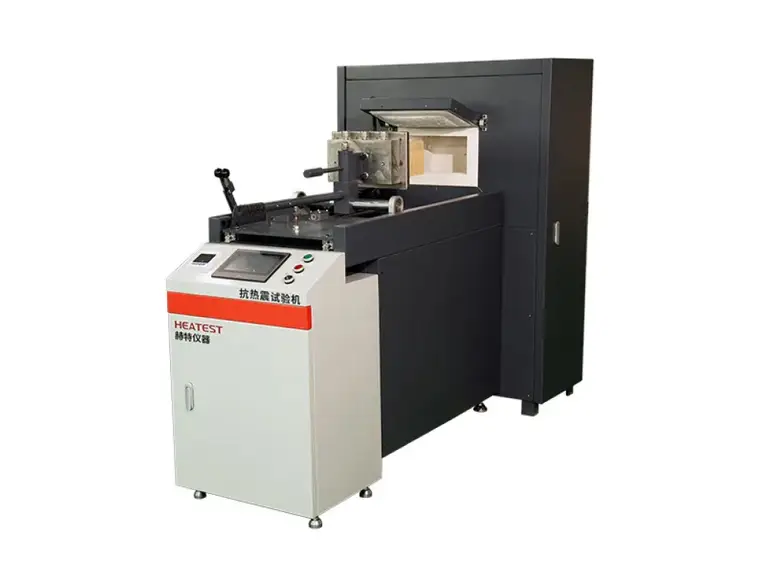
Electronics manufacturers and quality assurance engineers face an uncompromising demand: products must function flawlessly under extreme thermal stress. High temperature test equipment forms the backbone of reliability validation, exposing components to elevated temperatures that simulate worst-case operating scenarios or accelerated aging. Choosing the right system directly impacts product failure rates, time-to-market, and compliance with industry standards such as IEC 60068 or MIL-STD-810. This article provides a technical yet practical overview of high temp test equipment for electronics reliability testing, focusing on critical performance parameters, criterios de selección, and the advantages of partnering with a proven manufacturer like HEATEST Instrument.

Why High Temperature Testing Is Non‑Negotiable for Electronics

Electronic components and assemblies degrade faster when subjected to elevated temperature. Solder joints weaken, semiconductor junctions leak, dielectric materials lose insulation resistance, and thermal expansion mismatches cause mechanical fractures. High temperature testing accelerates these failure mechanisms, allowing engineers to identify weak points before mass production. Las aplicaciones comunes incluyen:

  • Burn‑in testing for ICs and power modules
  • Temperature cycling of PCBs to detect micro‑cracks
  • Storage life evaluation of batteries and capacitors
  • Endurance testing of relays, connectors, y sensores

Without proper high temp test equipment, manufacturers risk releasing products that fail prematurely in the field, leading to costly recalls and reputational damage. Reliability testing under controlled high‑temperature conditions is therefore a strategic investment, not merely a compliance checkbox.

Core Attributes of Reliable High Temp Test Equipment

Máquina de prueba de choque térmico

Not all thermal chambers are created equal. For electronics reliability testing, equipment must deliver precise, uniforme, and repeatable temperature environments. The following attributes separate professional‑grade solutions from basic ovens.

Uniformidad y estabilidad de la temperatura

The test volume must maintain temperature within tight tolerances (typically ±2°C or better) across all points. Poor uniformity leads to over‑testing some samples and under‑testing others, invalidating results. High‑end chambers employ multiple heating zones, high‑velocity air circulation, and optimized duct designs to achieve uniformity even at the upper limit of 300°C or beyond. HEATEST Instrument chambers are engineered with advanced airflow systems that guarantee ±1.5°C uniformity across the entire workspace.

…

Click here for more details on high-temperature testing equipment used for the reliability testing of electronic products: https://www.lyheatest.com/tester-knowledge/high-temp-test-equipment/

In high-temperature environmental testing, the temperature ramp rate—the speed at which a chamber heats or cools—often receives less attention than maximum temperature or chamber volume. Yet this parameter directly influences test reproducibility, product failure detection, and overall operational efficiency. A poorly controlled ramp rate can introduce thermal gradients, stress non-uniformity, and invalidate test results. Understanding why ramp rate matters is essential for selecting the right chamber and designing reliable accelerated life tests. This article explores the technical significance of ramp rate, the factors that determine it, y como Instrumento más caliente engineers chambers to deliver precise, repeatable thermal profiles.

What Is Temperature Ramp Rate?

Temperature ramp rate defines the speed of temperature change inside the test chamber, typically expressed in degrees Celsius per minute (°C/min). It can refer to the rate of heating (ramp-up) or cooling (ramp-down). While many specifications list a maximum ramp rate, the actual achievable rate depends on the chamber’s design, power capacity, and the thermal load presented by the test specimen.

Ramp-Up vs. Ramp-Down

Heating ramp rates are generally faster than cooling ramp rates because resistive heating elements can quickly add energy, while cooling requires refrigerant systems or liquid nitrogen to extract heat. In high-temp test chambers, ramp-down from extreme temperatures (p.ej., 300°C to room temperature) demands robust cooling subsystems. Instrumento más caliente optimizes both directions using advanced PID control and multi-stage refrigeration.

Why Temperature Ramp Rate Matters in High Temp Test Chambers

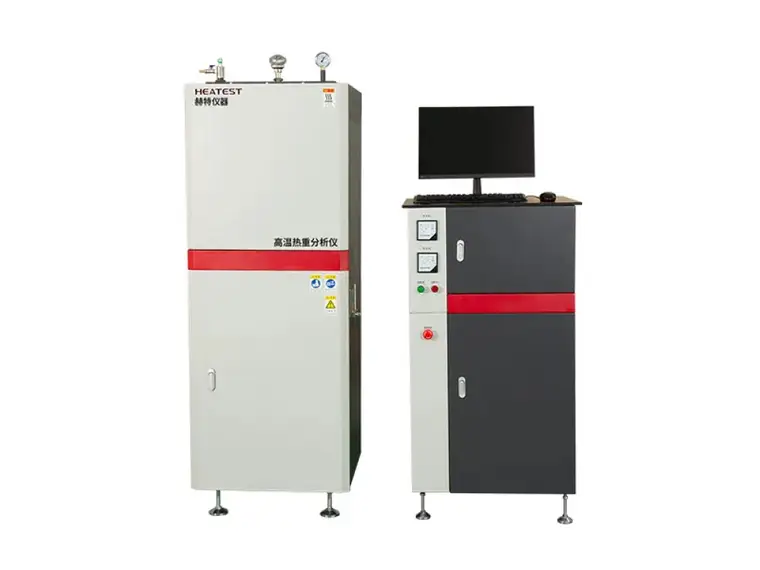
Analizador termogravimétrico

The ramp rate is not just a performance metric; it is a critical factor that affects test validity, product reliability, and cost of testing. Below are the key reasons why careful control of ramp rate is essential.

1. Impact on Thermal Gradient and Test Uniformity

When a chamber changes temperature too quickly, the air temperature near the heating elements or cooling coils may overshoot, creating spatial temperature gradients. Mientras tanto, the test specimen, often with high thermal mass, lags behind the air temperature. This mismatch causes surface-to-core temperature differences that can induce unrealistic thermal stresses. A controlled ramp rate ensures the specimen’s internal temperature follows the setpoint closely, maintaining uniform conditions throughout the workspace. HEATEST Instrument’s chambers incorporate high-efficiency air circulation and balanced heating/cooling zones to minimize gradients even during fast ramps.

…

Click here for more details on high-temperature testing equipment used for the reliability testing of electronic products: https://www.lyheatest.com/tester-knowledge/temp-ramp-rate-matters/

Selecting the right muffle furnace for ceramic sintering is a critical decision that directly affects product quality, eficiencia energética, y seguridad operativa. Ceramic materials demand precise thermal profiles, high-temperature uniformity, and robust construction to achieve consistent densification without defects. Whether you are setting up a new production line or upgrading an existing lab, understanding the technical specifications and design trade-offs is essential. This article breaks down the core factors you must evaluate before making a purchase, with practical insights grounded in industrial experience. As a trusted name in thermal processing equipment, Heatest Instrument offers reliable solutions tailored to ceramic sintering requirements.

Temperature Uniformity – The Cornerstone of Successful Sintering

In ceramic sintering, even minor temperature deviations can cause uneven shrinkage, pandeo, or incomplete densification. Por lo tanto, the furnace’s ability to maintain a consistent temperature across the entire work zone is paramount. When evaluating a muffle furnace, check the manufacturer’s stated uniformity rating, typically expressed as ±X°C within a specified volume at a setpoint. A quality furnace for ceramic applications should achieve ±3°C or better at peak temperatures (p.ej., 1600°C).

Several design aspects influence uniformity: insulation thickness, placement of heating elements, and airflow or convection management. High-end models use multiple independent heating zones controlled by separate thermocouples, allowing fine-tuning of the thermal gradient. Por ejemplo, Heatest Instrument’s advanced series features triple-zone PID control with dual feedback loops, ensuring that the temperature profile remains flat even during rapid heating or cooling cycles. Always request a temperature uniformity test report (usually per ASTM or AMS standards) before committing to a purchase.

Precision Temperature Control and Programmability

Ceramic sintering often requires complex ramp-up, soak, and cool-down profiles. A basic ON/OFF controller is insufficient; en cambio, look for a furnace equipped with a programmable PID controller that supports at least 16–24 segments of programmable steps. The controller should allow you to define heating rates (p.ej., 5°C/min for alumina, slower for silicon carbide), tiempos de espera, and cooling slopes.

Modern controllers also offer data logging via USB or Ethernet, enabling process traceability and quality assurance. For R&D environments, options like remote monitoring and recipe management are valuable. Heatest Instrument integrates Eurotherm or Honeywell controllers in its ceramic-specific furnaces, providing intuitive touchscreen interfaces and multi-language support. Verify that the controller’s accuracy (typically ±0.1°C) matches your process tolerance.

Heating Element Selection – Balancing Performance and Longevity

The heating element is the heart of the furnace. For ceramic sintering above 1200°C, common choices include molybdenum disilicide (MoSi2), carburo de silicio (Sic), and Kanthal Super. Each has distinct advantages and trade-offs:

…

Click here for more detailed information on key selection criteria for muffle furnaces used in ceramic sintering: https://www.lyheatest.com/electric-furnace-knowledge/muffle-furnace-guide-1/

Selecting the right temperature measurement method for high-temperature test equipment is critical to data reliability and process control. Two dominant approaches—infrared (IR) non-contact sensing and traditional contact-based thermocouples or RTDs—offer distinct trade-offs in accuracy, response speed, and applicability. This article provides a rigorous technical comparison of IR and contact measurement, helping engineers and procurement professionals make informed decisions for their specific thermal testing needs. Instrumento más caliente, a leading provider of high-temperature test equipment, offers solutions that leverage both technologies to meet diverse industry requirements.

Fundamental Differences Between IR and Contact Measurement

Understanding the operating principles is essential before evaluating performance. Contact measurement relies on physical contact between the sensor (thermocouple, IDT, or thermistor) and the test object. Heat transfers by conduction until thermal equilibrium, at which point the sensor temperature equals the object’s surface or internal temperature. En contraste, IR measurement uses a detector to capture thermal radiation emitted by the object’s surface, converting it to a temperature reading without physical contact.

Principle of Infrared (IR) Measurement

All objects above absolute zero emit infrared radiation proportional to their temperature. An IR sensor (pyrometer or thermal camera) focuses this radiation onto a detector, which outputs an electrical signal correlated to temperature. Key factors influencing accuracy include emissivity of the target surface, distance-to-spot ratio, and atmospheric absorption. Para aplicaciones de alta temperatura (por encima de 200°C), IR pyrometers are widely used in furnaces, foundries, and material testing because they do not disturb the thermal field and can measure moving or fragile objects.

Principle of Contact Measurement

Contact sensors require intimate thermal coupling with the test piece. Thermocouples, the most common type, generate a voltage based on the Seebeck effect at the junction of two dissimilar metals. RTD (resistance temperature detectors) change electrical resistance with temperature. Accuracy depends on proper installation, lead resistance compensation, and minimizing heat sinking effects. Contact probes are ideal for steady-state measurements in solid objects where surface access is possible and thermal disturbance is acceptable.

Comparación de rendimiento: Critical Parameters

Horno-de-prueba-de-refractariedad

To guide selection, the following table summarizes key performance differences between IR and contact measurement in high-temperature test equipment. These data reflect typical values under controlled laboratory conditions; actual performance may vary based on specific equipment and setup.

…

Click here for more detailed information on high-temperature testing equipment, covering both infrared and contact measurement methods: https://www.lyheatest.com/tester-knowledge/ir-vs-contact-measure/

Cold storage facilities and low-temperature warehouses present unique fire safety challenges due to subzero environments, dense insulation, and limited human occupancy. Unlike standard buildings, these spaces require specially engineered systems that can function reliably in extreme cold while maintaining strict temperature controls for stored goods. Understanding the essential fire protection components — from detection to suppression — is critical for warehouse managers, facility owners, and safety officers who must balance operational efficiency with life safety and property protection.

Understanding Fire Risks in Cold Storage Environments

Low-temperature warehouses create conditions that amplify certain fire hazards. The combination of polyurethane or polystyrene insulation panels (often combustible), electrical equipment in freezing conditions, and limited airflow can accelerate fire spread if not properly managed. Además, the extreme cold affects both the behavior of a fire — which may burn differently due to reduced oxygen or moisture — and the performance of conventional fire safety equipment. Por ejemplo, standard sprinkler systems may freeze, and detection devices can become sluggish. A thorough risk assessment should consider not only the stored commodities but also the building materials, refrigeration machinery, and maintenance practices unique to cold storage operations.

Essential Fire Protection Systems for Low-Temperature Warehouses

Effective cold storage fire safety relies on a layered approach combining active and passive systems. Below are the core components that every low-temperature warehouse should incorporate.

Sistemas de alarma y detección de incendios

Early detection is paramount, yet typical smoke detectors suffer from condensation and ice buildup in below-freezing environments. Specialized cold storage smoke detectors use heated housings or aspirating systems that sample air and warm it before analysis. Heat detectors remain a reliable alternative, but they must be rated for low-temperature operation. Integration with a central alarm system ensures rapid notification to on-site personnel and emergency responders. For unmanned facilities, automatic dialers or cellular alarms are recommended.

Sistemas de extinción de incendios

Suppression in cold storage involves unique engineering. Wet-pipe sprinkler systems are unsuitable because water in pipes can freeze and burst. El sellado superior e inferior de esta bolsa con válvula de fondo cuadrado no requiere costura, dry-pipe or pre-action sprinkler systems are used, where water is held back by a valve and released only after a detection event. These systems require careful design to prevent ice formation in pipes and to ensure adequate water flow in subzero temperatures. Clean agent suppression (p.ej., FM-200, Novec 1230) or inert gas systems are also viable options in confined areas such as electrical rooms or control panels, as they do not freeze and leave no residue. Sin embargo, they must be sized correctly to maintain oxygen levels safe for personnel.

Protección pasiva contra incendios

Building materials play a critical role. Insulation panels should be fire-rated with low flame spread indices y, ideally, include a metal facing that acts as a barrier. Compartmentalization using fire-rated walls and doors limits fire and smoke spread. All penetrations for pipes, cables, and ducts must be sealed with intumescent sealants that remain flexible at low temperatures. Además, emergency lighting and exit signage must be designed for freezing conditions and remain illuminated during power failures.

Key Challenges and Solutions for Cold Storage Fire Safety

Implementing these systems requires overcoming several technical hurdles specific to low-temperature warehouses.

Low Temperature Impact on Equipment

Batteries in alarm panels and emergency lights lose capacity in cold environments. Heated enclosures or remote location of sensitive electronics is necessary. similar, sprinkler system air compressors must be rated for continuous operation in freezers. Regular testing during winter months helps identify performance degradation before it leads to failure.

…

For more information on fire safety in cold storage—including details on the basic systems of low-temperature warehouses—please click here: https://www.tzykitchenware.com/a/news/cold-storage-fire-sa.html

Maintaining precise humidity in cold storage environments is a balancing act that directly impacts produce freshness, shelf life, y costos operativos. While many operators understand the importance of temperature control, the role of humidifiers is often misunderstood—leading to costly mistakes. This article separates common myths from scientific facts, offering a professional look at how humidifiers truly improve cold storage freshness. As a trusted supplier in the industry, TZY Kitchenware has helped numerous facilities optimize their humidity systems for better yields and reduced waste.

The Critical Role of Humidity in Cold Storage

Temperature alone cannot preserve freshness. When cold air circulates, it naturally loses moisture, causing dehydration in stored goods. Fruits and vegetables can lose 5–10% of their weight to water loss within days, even at optimal temperatures. This is where humidifiers become essential. By maintaining relative humidity (RH) Entre 85% y 95%, these devices slow transpiration, reduce shriveling, and maintain cellular structure.

How Low Humidity Damages Produce

  • Moisture loss: Leads to wilting, reducción de peso, and reduced market value.
  • Enzymatic browning: Dry conditions accelerate oxidation in cut fruits.
  • Microbial risk paradox: While high humidity can encourage mold, desigual humidity creates condensation hotspots that spoil produce faster.

Myth vs. Hecho: Common Misconceptions About Cold Storage Humidifiers

Over years of working with cold storage operators, TZY Kitchenware has identified repeated misunderstandings. Here are the most critical myths and their corresponding facts:

  1. Mito: Humidifiers are unnecessary if you have a modern refrigeration system.
    Hecho: Refrigeration inherently dries air. Even advanced systems remove moisture during cooling cycles. A dedicated humidifier is required to replenish lost humidity.
  2. Mito: Higher humidity always means better freshness.
    Hecho: Excess humidity (arriba 95% RH) can promote fungal growth. The optimal range varies by commodity—leafy greens prefer 90–95%, while root vegetables thrive at 85–90%.
  3. Mito: Ultrasonic humidifiers are best for cold storage.
    Hecho: While ultrasonic units are energy-efficient, they produce fine mist that may freeze or condense on cold surfaces. Evaporative or steam humidifiers are often more reliable for sub-40°F environments.
  4. Mito: Una vez instalado, a humidifier requires no maintenance.
    Hecho: Mineral buildup, biofilm, and clogged nozzles are common. Regular cleaning and water treatment are essential for consistent performance.

How Humidifiers Work in Cold Conditions: The Technology Explained

To achieve stable RH in a refrigerated space, the humidifier must overcome two challenges: cold air’s low moisture-holding capacity and the risk of freezing. Professional-grade units from manufacturers like TZY Kitchenware use one of three methods:

  • Steam injection: Boils water and injects vapor directly into air ducts. Provides precise control but requires energy and heated water supply.
  • Evaporative (pad) sistemas: Pass air through wetted media. Simple and economical, but pad replacement is needed periodically.
  • High-pressure misting: Fine droplets evaporate quickly. Suitable for large warehouses, but nozzle clogging can be an issue.

…

Click here for more detailed information—including myths and facts—on how humidifiers enhance the freshness of refrigerated foods: https://www.tzykitchenware.com/a/news/humidifier-cold-stor.html

Maximizing the number of pallets stored in a cold environment directly impacts operational efficiency and cost per unit. Sin embargo, every additional pallet and rack level introduces a risk: restricted airflow can create temperature gradients, cause product dehydration, or even lead to microbial growth. The challenge is not merely to pack more pallets into the same footprint, but to do so while maintaining uniform air circulation across all storage zones. This article dissects the engineering principles behind high-density cold storage and presents actionable solutions—leveraging TZY Kitchenware’s proven racking systems—that allow you to increase density without compromising your cold chain integrity.

Understanding the Trade-Off: Density vs. flujo de aire

Cold storage relies on continuous, even airflow to remove heat and maintain a stable set-point temperature. When pallets are arranged with minimal gaps, air can bypass certain lanes, creating dead zones. Standard 48-inch deep selective racking, por ejemplo, typically allows good airflow but uses only about 25-30% of the available floor space for pallet positions. High-density systems like drive-in or push-back racks can boost space utilization to 60-70%, but they inherently reduce the number of open air passages. The key is to design the rack geometry, pallet overhang, and ventilation slots so that air is forced to flow through, not around, the stored product.

Key Strategies for Density Without Compromise

Rack Design with Integrated Air Channels

Innovative rack profiles now include perforated beams or wire decks that allow vertical airflow. Menaje de cocina TZY recommends using rack uprights with slotted openings and deep beam channels that create a natural air plenum. For drive-in systems, we specify vented back-to-back uprights that direct air from the refrigeration floor nozzles upward through the pallet rows. This design allows you to stack pallets three or four high while maintaining a temperature variance of less than 2°C across all levels.

Strategic Lane Depths and Pallet Orientation

In deep-lane systems, reducing the lane depth from 12 a 8 pallets can significantly improve air movement. For every additional pallet deep, the pressure drop increases exponentially. By limiting lane depth to 8 pallets and orienting pallets so that the longer side faces the airflow (turning block-stacked pallets 90 grados), you can achieve 90% of theoretical density while retaining 85% of airflow effectiveness. TZY Kitchenware’s layout software calculates optimal lane depth based on your specific product dimensions and refrigeration airflow CFM.

Automated Storage and Retrieval (ASRS) with Tilted Shelves

For very high density (arriba a 40% more than standard racks), ASRS systems with tilted shelves (p.ej., 2-3 grados) allow air to flow along the sloped surface, reducing stagnation. Combined with a low-velocity ceiling-mounted fan system that runs at 0.5 EM, this configuration prevents moisture condensation on goods without increasing energy consumption. TZY Kitchenware partners with automation providers to integrate these tilt mechanisms into standard rack modules.

…

Click here for more details on maximizing cold storage pallet density without compromising air circulation: https://www.tzykitchenware.com/a/news/cold-storage-pallet-.html

Every commercial cold storage facility eventually faces the same critical question: should you invest in repairing an aging cooler, or is it time to budget for a full replacement? The decision impacts not only operational costs but also energy efficiency, food safety compliance, and long-term asset management. Understanding the lifecycle of your cooling equipment and recognizing the telltale signs of wear can save your business thousands of dollars and prevent unexpected downtime. This guide provides a structured framework for evaluating repair versus replacement scenarios, drawing on real-world performance data and industry best practices.

Understanding the Cold Storage Lifecycle and Key Aging Indicators

Industrial coolers typically have a designed lifespan of 10 a 15 años, depending on duty cycles, ambient conditions, and maintenance history. As equipment approaches this age range, performance degradation becomes inevitable. The first step in making an informed decision is to objectively identify where your cooler stands in its lifecycle.

Common Signs of Cooler Degradation

  • Compressor cycling issues: Frequent on/off cycling or prolonged run times indicate declining compressor efficiency or oversized components.
  • Refrigerant leaks: Minor leaks that require more than annual top-ups suggest failing seals or microcracks in the evaporator coil.
  • Heat exchanger fouling: Reduced heat transfer due to corrosion, escombros, or scaling on condenser coils lowers overall system performance.
  • Controller errors: Outdated or malfunctioning electronic controllers cause temperature swings that can compromise product quality.

The Role of Preventive Maintenance in Extending Life

Regular maintenance—including coil cleaning, refrigerant pressure checks, and belt replacements—can push the functional lifespan beyond the average. Sin embargo, after the 12-year mark, even well-maintained coolers often suffer from a cumulative decline in energy efficiency. A study from the Food Service Technology Center indicates that systems older than 12 years can consume 20-30% more electricity than modern Energy Star-rated units.

Repair vs. Reemplazar: A Cost-Benefit Analysis

Evaluating the financial case requires looking beyond the immediate repair invoice. A comprehensive approach should factor in energy savings, frecuencia de mantenimiento, and risk of catastrophic failure. Below is a structured comparison of the key decision factors.

  • Annual repair cost vs. 10% of replacement cost: If your cooler requires repairs exceeding 50% of the price of a new unit, replacement is almost always more economical. Sin embargo, even smaller recurring repairs—for example, three service calls per year—should prompt a lifecycle cost analysis.
  • Consumo de energía: Modern coolers use variable-speed compressors and high-efficiency fans. Switching from a 10-year-old unit to a new one can yield 15-25% energy savings annually, often offsetting the capital cost within 3-4 años.
  • Reliability and downtime risk: A unit that has failed twice in six months has a high probability of future breakdowns. The cost of lost inventory due to temperature excursions should be weighted heavily in the decision.
  • Compliance and sustainability: Newer models typically use environmentally friendlier refrigerants (p.ej., R-290 or R-448A) and comply with updated emissions standards. Repairing an R-22 system may involve expensive, phased-out refrigerant.

…

For more detailed information on the service life of cold storage facilities—including when to repair aging units versus when to replace them—please click here: https://www.tzykitchenware.com/a/news/cold-storage-repair-.html

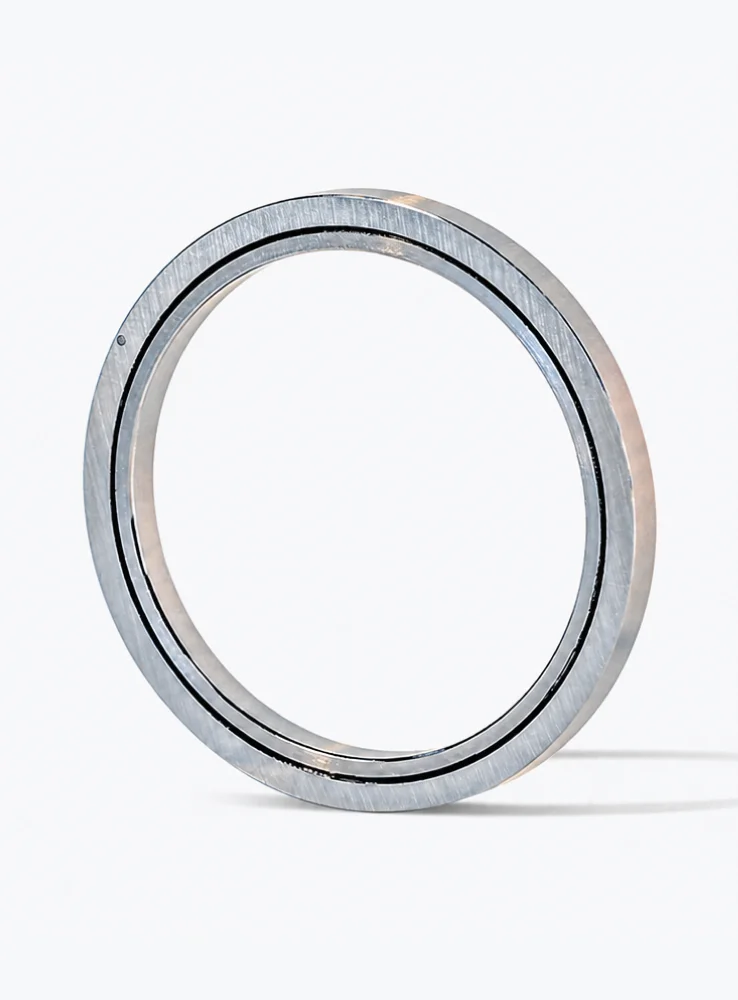
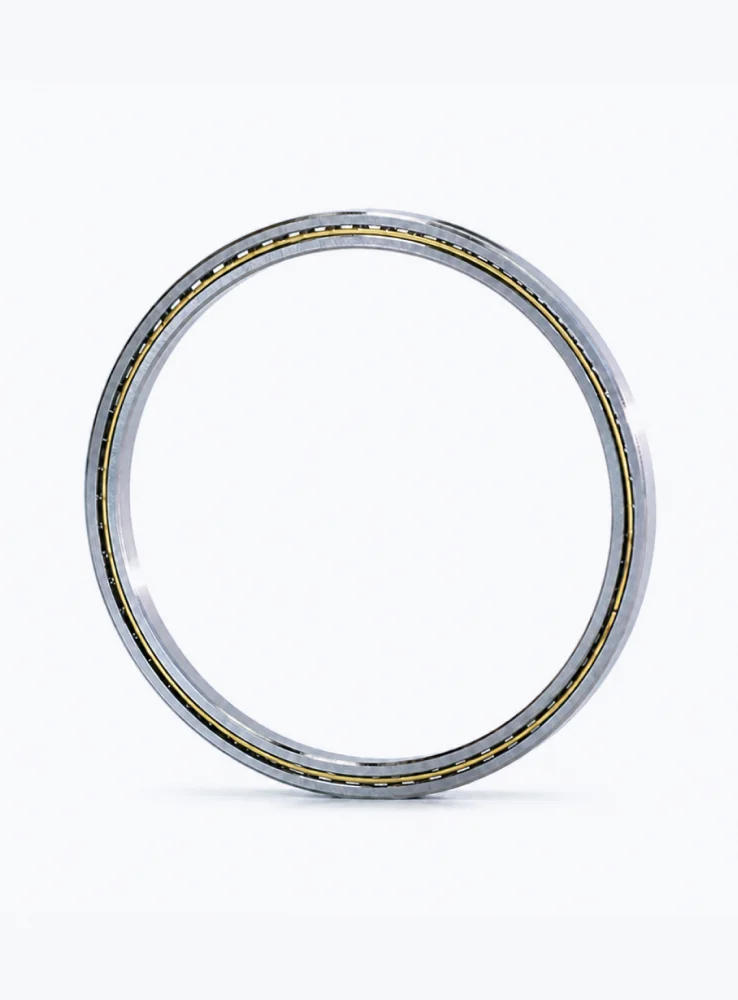
Crossed roller bearings are precision components that deliver exceptional rigidity and rotational accuracy in demanding applications such as robotics, Equipo medico, and machine tool turrets. Sin embargo, even the best engineered bearing will fail prematurely if common mistakes are made during selection, instalación, lubricación, o mantenimiento. Understanding these pitfalls is essential for maximizing service life, avoiding costly downtime, and ensuring that your machinery operates at peak performance. This article highlights the most frequent crossed roller bearing errors and provides practical guidance to help you steer clear of them.

Error #1: Incorrect Bearing Selection for the Application

The foundation of reliable bearing performance starts with choosing the right bearing type and size. Many engineers underestimate the complexity of crossed roller bearings, which leads to suboptimal selection and eventual failure.

Ignoring Load Direction and Magnitude

Crossed roller bearings can handle combined axial, radial, y cargas de momento, but their capacity varies with the direction and distribution of the load. A common mistake is selecting a bearing based solely on radial load capacity without calculating the actual moment loads generated by cantilevered or offset masses. This oversight can result in premature fatigue or raceway brinelling. Always evaluate the full load spectrum, including shock loads, and consult the bearing manufacturer’s rating tables for the equivalent dynamic load under combined loading conditions.

Overlooking Rotational Accuracy Requirements

Applications like indexing tables and rotary encoders demand very tight runout and positioning accuracy. Selecting a standard crossed roller bearing when a higher accuracy class (such as P5 or P4) is required can lead to unacceptable error in the system. Si el tractor puede cambiar de marcha en el momento oportuno, overspecifying accuracy without need drives up cost. Match the bearing precision grade to the actual performance requirements of your equipment.

Error #2: Poor Mounting and Housing Fit

Even the most precise crossed roller bearing will perform poorly if it is installed in a housing or on a shaft with incorrect fits. Improper interference or clearance affects the internal clearance of the bearing, which in turn alters contact stress and can cause skidding or excessive heat.

Incorrect Tolerance of Mating Surfaces

Machining the housing bore or shaft to the wrong tolerance is one of the most common installation mistakes. If the fit is too tight, the crossed roller bearing’s internal clearance is reduced, leading to increased friction and heat generation. If the fit is too loose, the bearing can creep, causing wear on the housing and shaft, and eventually resulting in misalignment. Always follow the manufacturer’s recommended shaft and housing tolerances for the specific bearing series.

Using the Wrong Mounting Method

Crossed roller bearings are often split into two-piece or three-piece designs. Some installers attempt to press the entire bearing on the shaft using force that bypasses the rolling elements, which can damage the raceways. El sellado superior e inferior de esta bolsa con válvula de fondo cuadrado no requiere costura, use the proper mounting sleeves or apply uniform pressure on the inner ring when mounting onto a shaft. For thin-wall bearings, avoid using direct hammering; use a suitable press or a hydraulic expansion tool to avoid distortion.

Error #3: Neglecting Proper Lubrication

Lubrication is the lifeline of any bearing, and crossed roller bearings are no exception. Incorrect lubrication or inadequate quantities are leading causes of premature bearing failure.

Using the Wrong Grease or Oil

Crossed roller bearings operate at various speeds, temperatures, and load conditions. Using a grease with insufficient viscosity or a base oil that is not compatible with the operating environment can lead to poor film formation and metal-to-metal contact. Para aplicaciones de alta velocidad, a low-viscosity oil circulating system may be required, while low-speed high-load applications benefit from high-viscosity grease with EP (extreme pressure) aditivos. Always consult the bearing manufacturer or a lubrication engineer to choose a lubricant that matches the specific operating conditions.

Over-Lubrication or Under-Lubrication

Too much grease can cause churning, which raises the temperature and degrades the lubricant. Too little grease leaves the bearing unprotected. Many lubrication schedules are based on general estimates rather than actual operating hours. Implement a defined preventive maintenance schedule that specifies the correct volume and interval for regreasing, based on the bearing’s operating time and environment. For sealed crossed roller bearings, the initial lubrication is often life-long, but only if the correct amount is pre-filled; do not attempt to regrease sealed units unless instructed.

Error #4: Improper Handling and Storage

Crossed roller bearings are machined to tolerances of a few micrometers. Mishandling or poor storage can damage these components before they are ever installed.

Exposing Bearings to Contamination

Polvo, humedad, and abrasive particles are the enemies of precision bearings. Leaving bearings unboxed on a dirty workbench, using contaminated tools, or failing to clean the surrounding area before installation can introduce particles that cause early wear. Always keep bearings in their original packaging until installation, and use clean, lint-free cloths and gloves when handling.

…

Click here for more detailed information on avoiding these common cross-roller bearing errors: https://www.bobibearing.com/a/bearing-knowledge/crossed-roller-mistakes.html