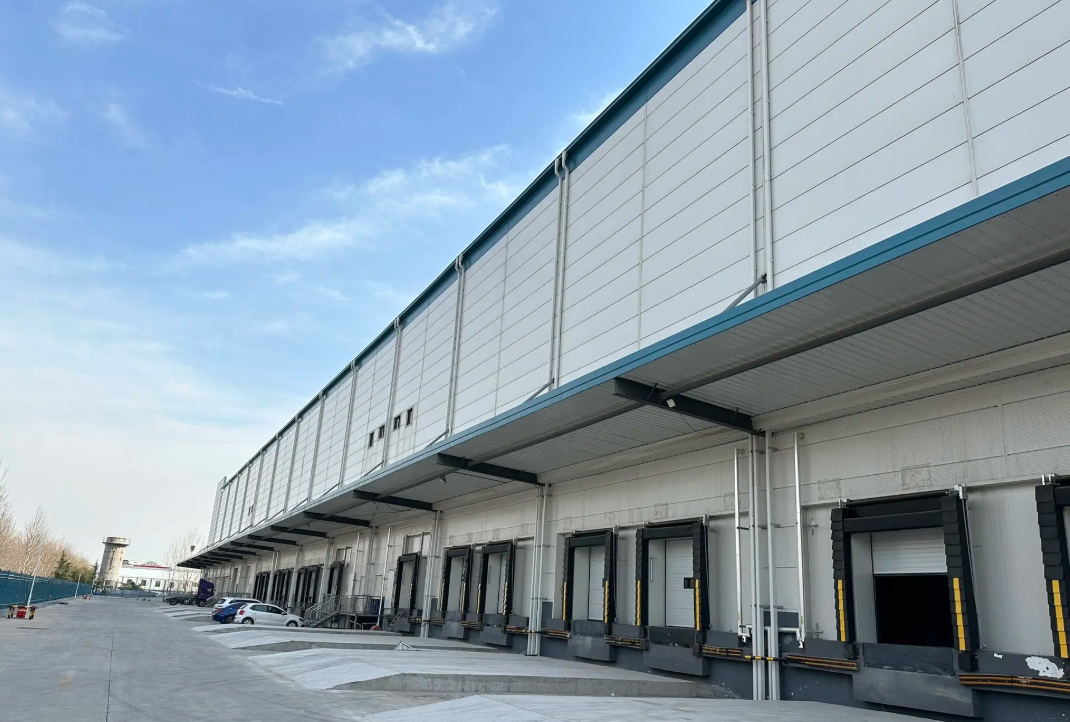
Industrial expansion demands speed, scalability, and cost control—three factors that traditional construction often fails to deliver. Modular steel buildings have emerged as a game-changing alternative, enabling businesses to add capacity in months rather than years while maintaining structural integrity and flexibility. This shift is not merely a trend; it represents a fundamental rethinking of how industrial space is created, and companies like MeiChen Steel are at the forefront of engineering these solutions. Understanding why modular steel buildings are revolutionizing industrial expansion can help decision-makers evaluate whether this approach aligns with their growth strategies.

The Growing Need for Agile Industrial Expansion

Manufacturing, logistics, and energy sectors face relentless pressure to scale quickly. Supply chain disruptions, fluctuating demand, and the rise of e-commerce have made agility a competitive imperative. Traditional site-built construction—with its permitting delays, weather dependencies, and labor shortages—often creates bottlenecks that hamper growth. Modular steel buildings address these pain points by shifting most fabrication off-site into controlled factory environments, where production runs parallel to site preparation. This parallel process can cut overall project timelines by 30% to 50% compared to conventional methods, a critical advantage when market windows are narrow.

What Makes Modular Steel Buildings Different?
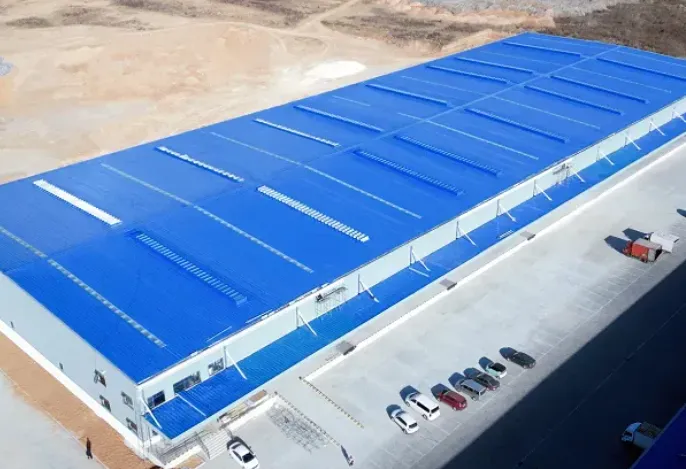
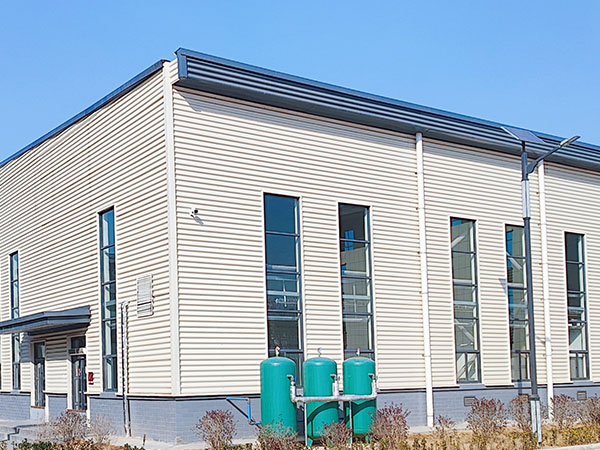
Modular steel buildings

Off-Site Fabrication, On-Site Assembly

Unlike stick-built structures, modular steel buildings are composed of prefabricated sections—walls, roof panels, and integrated systems—manufactured to precise specifications in a factory. These modules are then transported to the site and assembled rapidly. The process reduces waste, improves quality control, and eliminates many of the variables that slow down traditional builds. MeiChen Steel specializes in designing modules that can be customized to fit specific industrial layouts, from warehouse expansions to multi-story production facilities.

Inherent Flexibility for Future Changes

Industrial requirements rarely stay static. A building that works for today’s production line may need reconfiguration next year. Modular steel systems are inherently adaptable: non-load-bearing walls can be repositioned, modules can be added or removed, and the open-span design allows for large, column-free interiors. This flexibility reduces long-term capital risk and supports continuous process improvement—a key reason why forward-thinking facility managers are embracing modular approaches.

Key Advantages Over Traditional Construction

The revolution in industrial expansion is driven by measurable benefits that go beyond speed. Below is a comparison between modular steel buildings and conventional construction across critical decision factors:

  • Schedule: Modular projects typically complete 30–50% faster because site work and module fabrication happen concurrently.
  • Cost Certainty: Factory-controlled production minimizes change orders and material waste, providing tighter budget control. Traditional projects often experience 10–20% cost overruns due to unforeseen site conditions or delays.
  • Quality: Modules are built under consistent conditions with rigorous inspections, resulting in fewer defects. On-site construction is subject to weather, trades coordination issues, and inconsistent workmanship.
  • Safety: Less on-site work means fewer opportunities for accidents. Factory settings have established safety protocols and reduced exposure to heights and heavy equipment.
  • Sustainability: steel is infinitely recyclable, and off-site fabrication generates significant waste reduction—up to 70% less scrap compared to traditional methods. Energy efficiency can be optimized during design.
  • Scalability: Modules can be sized for standard truck transport, allowing phased expansions that align with budget cycles and demand growth.

Addressing Common Concerns

Some decision-makers worry that modular buildings look utilitarian or limited in design. In reality, modern modular steel structures can incorporate architectural features, insulation systems, and finishes that match or exceed traditional buildings. Additionally, financing and permitting are often streamlined because modular systems comply with recognized building codes (IBC, ASTM, AISC) just as site-built structures do. MeiChen Steel provides engineering documentation and third-party certifications to ensure seamless approval processes.

…

For more details on why modular steel construction is revolutionizing industrial expansion, please click here: https://www.meichensteel.com/a/procurement-guides/modular-steel-guide.html
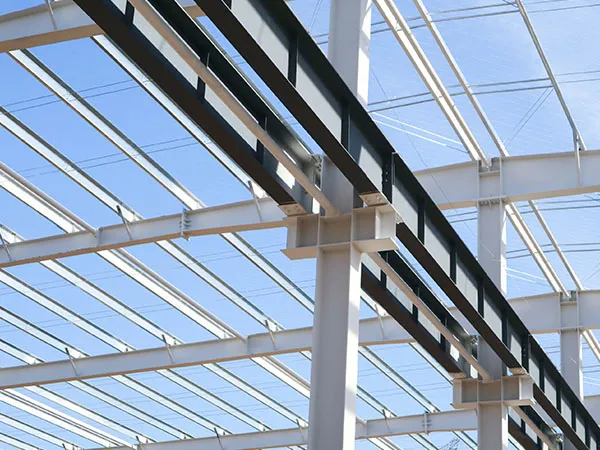
Steel structures form the backbone of modern infrastructure, from high-rise buildings to industrial bridges. Understanding load-bearing capacity is critical for engineers, architects, and project owners who must ensure safety, longevity, and cost-efficiency. This article breaks down the engineering principles behind steel structure load capacity, including material behavior, design factors, and real-world applications. Whether you’re specifying a new project or evaluating existing construction, the insights here will help you make informed decisions—and show how partners like MeiChen Steel deliver reliable solutions.

Fundamentals of Load-Bearing Capacity in Steel Structures

The load-bearing capacity of a steel structure is its maximum ability to resist applied forces without failure. This depends on three core elements: material strength, cross-sectional geometry, and structural stability. Steel is favored for its high strength-to-weight ratio, ductility, and uniformity compared to concrete or timber.

Stress and Strain: The Building Blocks

When a load is applied, steel experiences stress (force per unit area) and strain (deformation). The yield point—where steel begins to deform permanently—is a key design limit. For most structural steel grades like ASTM A36 or A992, yield strength ranges from 250 MPa to 345 MPa. Engineers design structures to remain below this limit under service loads, ensuring elastic behavior.

Cross-Section and Section Modulus

The shape of a steel member dramatically affects its load capacity. An I-beam, for example, has a high section modulus, meaning it resists bending efficiently. A wider flange increases stiffness without proportional weight gain. The section modulus (S) and moment of inertia (I) are calculated from geometry and used in bending stress formulas: σ = M / S.

Key Factors Affecting Load-Bearing Capacity

Steel Structures

Several interrelated factors determine the final capacity of a steel structure. Ignoring any can lead to underperformance or failure.

  • Steel Grade and Material Properties: Higher yield strength (e.g., 420 MPa vs. 250 MPa) allows thinner sections, but may reduce ductility. Choose a grade that matches your load and seismic requirements.
  • Cross-sectional Geometry: Wide-flange shapes, hollow structural sections (HSS), and built-up plate girders each offer different capacities for axial, bending, and torsional loads.
  • Connection Design: Bolted or welded connections must transfer forces without local failure. Connection details often govern the ultimate capacity of a truss or frame.
  • Bracing and Stability: Buckling—both local (flange/web) and global (flexural-torsional) —can reduce capacity drastically. Proper bracing and stiffeners are mandatory.
  • Loading Conditions: Dead loads (self-weight), live loads (occupancy), wind, snow, and seismic forces combine. Load combinations are codified in standards like ASCE 7 or EN 1990.

Engineering Calculations and Safety Factors

Design codes (AISC 360, Eurocode 3) use load and resistance factor design (LRFD) or allowable strength design (ASD). In LRFD, factored loads are compared with nominal strength reduced by a resistance factor (e.g., φ = 0.9 for bending). This accounts for material variability, modeling uncertainties, and construction tolerances.

A typical design sequence: 1) Determine required strength from load combinations. 2) Select trial member. 3) Check axial capacity (P_n), flexural capacity (M_n), shear capacity (V_n). 4) Verify combined stresses (biaxial bending + axial). 5) Check deflection serviceability (L/360 or tighter for sensitive structures).

For example, a W10x49 column in A992 steel (F_y = 345 MPa) with unbraced length 3 meters may have an axial capacity of approximately 1,800 kN in LRFD, considering slenderness ratio and buckling curve. Actual values require detailed computation—never rely on rules of thumb alone.

How to Ensure Maximum Load-Bearing Capacity in Your Project

Steel Structures

Beyond theoretical calculations, practical execution determines real-world performance.

  • Specify Certified Steel: Always use material with mill test reports verifying grade, yield, tensile strength, and elongation. MeiChen Steel provides full traceability for all carbon and high-strength steel products.

…

For more detailed information on the load-bearing capacity of steel structures—including an in-depth explanation of the engineering principles—please click here: https://www.meichensteel.com/a/procurement-guides/load-bearing-capacity-of-steel-structures.html

Coastal environments present one of the most aggressive challenges for steel buildings. Constant exposure to salt-laden air, high humidity, and frequent moisture cycles accelerates corrosion, leading to structural degradation if left unaddressed. For property owners and facility managers along coastlines, understanding how to properly protect a steel building is not just about aesthetics—it is a critical investment in safety, longevity, and long-term cost savings. This guide provides a professional, actionable framework for mitigating corrosion risks, with insights drawn from industry best practices and the expertise of MeiChen Steel, a trusted name in steel structure solutions.

Understanding the Corrosion Challenge in Coastal Environments

Corrosion is an electrochemical process that occurs when steel reacts with oxygen and moisture. In coastal areas, the presence of chloride ions from sea salt dramatically accelerates this reaction. Even steel buildings located miles inland can be affected due to prevailing winds carrying salt spray. The result is pitting, rust formation, and eventual loss of structural integrity if preventive measures are not implemented from the design phase onward.

How Saltwater and Humidity Accelerate Corrosion

Salt particles dissolve in water to form a conductive electrolyte that facilitates electron flow between anodic and cathodic sites on the steel surface. This increases the corrosion rate by a factor of 5 to 10 compared to inland environments. High relative humidity—often above 80% in coastal zones—keeps the metal surface wet for longer periods, further accelerating the process. The combination of temperature fluctuations and UV radiation can also degrade protective coatings over time, exposing the base metal.

Unique Risks for Steel Buildings

Steel buildings have numerous joints, fasteners, and overlapping panels where moisture can become trapped. Crevice corrosion and galvanic corrosion between dissimilar metals (e.g., steel fasteners against aluminum sheeting) are common failure points. Roof valleys, gutters, and areas near HVAC units are particularly vulnerable because they collect debris and retain moisture. A comprehensive protection plan must address all these micro-environments.

Key Protective Measures for Steel Buildings

steel buildings

Effective corrosion protection is a multi-layered strategy. No single solution is sufficient; instead, combine material selection, surface treatment, coating systems, and ongoing maintenance to achieve maximum service life.

Proper Material Selection

Start by choosing steel grades with inherent corrosion resistance. Galvanized steel with a thick zinc coating (e.g., G90 or higher) provides sacrificial protection. For extreme coastal exposure, consider 55% aluminum-zinc alloy coated steel (e.g., Galvalume), which offers 2-4 times the corrosion resistance of standard galvanized steel. Stainless steel (such as 316 grade) is an option for critical structural components, though at a higher cost. MeiChen Steel recommends evaluating the specific environmental severity before finalizing material specifications.

Protective Coatings and Paints

A properly applied coating system is the primary barrier against salt and moisture. The system should include a primer with corrosion-inhibiting pigments (e.g., zinc-rich epoxy) followed by a durable topcoat (polyurethane or silicone-modified polyester). Key factors for success include:

  • Surface preparation: Abrasive blasting to achieve a clean, profiled surface (e.g., SSPC-SP10 near-white metal blast) is essential for coating adhesion.
  • Dry film thickness: Apply a minimum of 3-4 mils primer plus 2-3 mils topcoat for coastal zones; thicker for critical areas.
  • Edge and fastener protection: All sharp edges should be rounded and coated, and exposed fasteners should be covered with sealing caps or mastic.

Regular Maintenance and Inspection

No coating lasts forever. Establish a scheduled inspection program—at least twice per year—to identify early signs of coating failure, such as cracking, blistering, or rust bloom. Promptly repair any damaged areas by spot-blasting and recoating. Additionally, keep gutters clean and trim vegetation away from the building to reduce moisture retention. A well-maintained building can extend its corrosion-free life by decades.

…

For more detailed information on how to protect steel structures in coastal areas from corrosion, please click here: https://www.meichensteel.com/a/procurement-guides/protect-steel-building-from-corrosion-in-coastal-areas.html

Industrial steel buildings integrated with crane systems represent a strategic investment for manufacturing, warehousing, and logistics operations that require heavy lifting capacity within a controlled environment. Unlike traditional construction methods where cranes are retrofitted after building completion, integrated crane systems are engineered into the steel framework from the initial design phase, ensuring structural compatibility, load distribution optimization, and long-term operational efficiency. This article examines the critical design considerations, comparative advantages, and practical implementation aspects of such facilities, while highlighting how MeiChen Steel delivers turnkey solutions that balance strength, cost, and versatility.

Design Philosophy: Structural Integration from Day One

The core principle behind an integrated crane system is that the building frame and the crane support structure act as a single unified system. This integration offers several mechanical and economic benefits compared to post-installation modifications.

Load Path Optimization

In a conventional building, a crane system is supported by separate columns or roof trusses added after the main structure is erected. This often leads to redundant load paths, increased steel tonnage, and potential stress concentrations. In contrast, an integrated design uses the building’s main columns and rafters as direct crane supports. The crane runway beams are attached to column brackets or cap plates that are shop-welded or bolted, distributing the vertical and horizontal crane loads efficiently into the foundation. MeiChen Steel’s engineering team performs finite element analysis to ensure that every connection point handles the specified crane capacity without over-stressing the primary frame.

Clear Span vs. Multi-Span Configurations

Industrial buildings with integrated cranes typically adopt clear span (rigid frame) or multi-span (interior columns) layouts. Clear span designs eliminate interior columns, providing unobstructed floor space ideal for large cranes that travel the entire bay length. Multi-span designs, while reducing individual girder sizes, require careful coordination of runway beams across multiple bays. For facilities requiring multiple cranes operating in the same bay, MeiChen Steel recommends multi-span configurations with interlocking crane bridges to maximize throughput.

Core Advantages of Integrated Crane Systems

When comparing integrated crane buildings to retrofit installations, several distinct benefits emerge, directly impacting project timelines, operational costs, and safety margins.

  • Reduced construction cost: By eliminating redundant steel members and simplifying foundation design, integrated projects typically save 10–15% in structural steel costs compared to a non-integrated equivalent.
  • Shorter project schedule: Engineering and fabrication proceed simultaneously for building and crane components from the same design database, cutting overall delivery time by 4–8 weeks.
  • Enhanced seismic performance: Integrated frames can be designed as moment-resisting systems that work in concert with the crane mass during earthquakes, reducing the risk of crane derailment.
  • Future upgrade flexibility: MeiChen Steel designs runway beams with extra capacity margin (typically 10–15%) and bolted connections that allow lighter cranes to be replaced with heavier models without major structural modifications.
  • Improved worker safety: Integrated systems eliminate the need for field welding of crane supports at height, reducing fall hazards. Pre-engineered attachment points also simplify future maintenance access.

…

For more details on why crossed-roller slewing bearings excel in high-precision applications, please click here: https://www.meichensteel.com/a/procurement-guides/steel-buildings-crane-systems.html

In precision machinery, the choice of slewing bearing directly determines positioning accuracy, repeatability, and long-term stability. Cross-roller slewing bearings have emerged as the preferred solution for demanding applications such as semiconductor manufacturing, medical imaging, and precision rotary tables. Their unique roller arrangement provides superior moment stiffness and rotational accuracy compared to conventional ball-type bearings. This article examines the engineering principles behind their performance, compares them with alternative designs, and explains why cross-roller bearings—especially those manufactured by LYMC—are the optimal choice when sub-arcminute accuracy is required.

The Structural Advantage of Cross-Roller Slewing Bearings

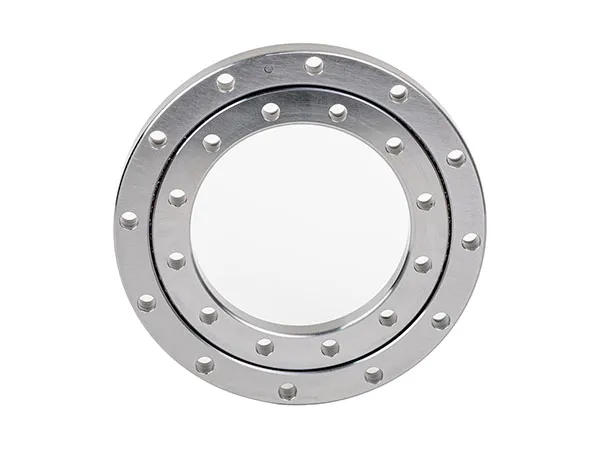
Unlike single-row ball slewing rings, cross-roller bearings arrange cylindrical rollers in a crisscross pattern at a 90° angle between two adjacent rollers. This configuration provides equal load capacity in all radial, axial, and moment directions. Each roller is separated by a spacer, eliminating friction between adjacent rollers and reducing heat generation. The line contact between rollers and raceways distributes stress over a larger area, resulting in significantly higher static and dynamic load ratings compared to ball contacts of equivalent size.

Preload and Rigidity

Cross-roller bearings are typically supplied with a negative internal clearance (preload) tailored to the application. This preload removes all axial and radial play, ensuring that the bearing behaves like a solid ring under load. The result is high system stiffness, which is critical for maintaining positional accuracy under varying cutting forces or torque loads. In contrast, ball-type slewing rings often require external preloading devices or serrated locking mechanisms to achieve similar rigidity.

Comparison: Cross-Roller vs. Other Slewing Bearing Types

slewing bearing

To understand why cross-roller bearings excel, it is useful to compare them directly against common alternatives used in high-precision tasks.

  • Single-row 4-point contact ball bearings: These bearings rely on point contact, which limits moment stiffness. Under combined loads, ball deformation increases friction and reduces rotational accuracy. Cross-roller bearings offer 3–5× higher moment rigidity in a comparable envelope.
  • Double-row ball slewing rings: While they improve load capacity over single-row designs, the balls still produce point contact. The axial preload needed to eliminate play increases wear and limits service life. Cross-roller bearings maintain consistent torque over thousands of cycles with minimal wear.
  • Wire-race bearings: These are lighter but less rigid. Their steel wires deform under high dynamic loads, making them unsuitable for sub-micron repeatability. Cross-roller bearings, manufactured from hardened bearing steel (e.g., SUJ2 or 50CrMo4), provide dimensional stability over temperature variations.

Key Performance Parameters in High-Precision Tasks

When evaluating a slewing bearing for tasks such as wafer handling, laser cutting, or optical alignment, engineers focus on four metrics:

  1. Running accuracy (TIR): Cross-roller bearings achieve axial runout values below 5 µm when installed correctly. This is due to the precision-ground raceways and matched roller sets.
  2. Friction moment uniformity: The roller-cage assembly ensures low and consistent starting torque, essential for servo-driven rotary axes that require smooth motion at low speeds.
  3. Life under continuous oscillation: Many high-precision applications involve partial rotation (e.g., ±90°). Cross-roller bearings excel here because the line contact distributes wear evenly across the raceway surface, preventing brinelling common with ball bearings.
  4. Thermal stability: Because cross-roller bearings generate less heat than sliding bearings or heavily preloaded ball bearings, they maintain their geometry over long operating periods. LYMC uses advanced heat treatment processes to achieve Rockwell hardness of HRC 58–62 on raceways, ensuring consistent performance even in temperature-controlled cleanrooms.

…

For more details on why crossed-roller slewing bearings excel in high-precision applications, please click here: https://www.mcslewingbearings.com/a/news/cross-roller-precision.html

Selecting the correct slewing bearing is a critical engineering decision that directly affects equipment performance, safety, and longevity. A miscalculation in sizing can lead to premature failure, costly downtime, or even catastrophic structural damage. This guide provides a systematic approach to slewing bearing sizing, helping you align technical parameters with your specific application requirements. Whether you are designing new equipment or replacing an existing bearing, understanding the fundamentals of load calculation, geometry, and environmental considerations is essential. With decades of industry expertise, LYMC offers precision-engineered slewing bearings tailored to diverse industrial needs, ensuring reliability and optimal operational efficiency.

Understanding Load Requirements for Slewing Bearings

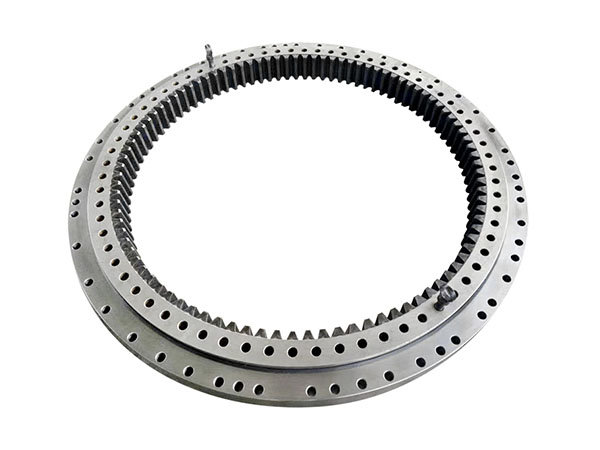
The first and most critical step in slewing bearing sizing is accurately determining the loads the bearing will encounter during operation. Slewing bearings typically handle three primary load types: axial load (thrust), radial load, and tilting moment. These loads are rarely static; they vary with dynamic conditions such as acceleration, deceleration, wind, and payload shifts.

Axial Load (Thrust Load)

Axial load acts parallel to the bearing’s axis of rotation. For example, in a crane, the weight of the crane itself plus the lifted load creates an axial force. When calculating, include both the static weight of the rotating structure and any live loads. Use the maximum expected load in worst-case scenarios.

Radial Load

Radial loads act perpendicular to the bearing axis. These are often generated by side forces from wind, rope tension, or misalignment. Many slewing bearings are designed primarily for axial loads and tilting moments, but radial loads must still be accounted for—especially in applications like excavators or wind turbines where lateral forces are significant.

Tilting Moment

The tilting moment is the most complex and often the dominant factor in slewing bearing selection. It results from loads applied at a distance from the bearing center, creating a bending moment that tries to tilt the rotating platform. The formula for tilting moment is load multiplied by the distance from the bearing center (lever arm). Always consider the combination of all loads acting simultaneously to determine the worst-case tilting moment.

Tip: Use safety factors of 1.25 to 2.0 depending on application criticality and operating conditions. LYMC recommends consulting their engineering team for custom load analysis using finite element methods.

Key Sizing Parameters: Geometry and Performance

Slewing Bearing

Once loads are established, the next step involves matching bearing geometry to your equipment’s physical constraints and performance requirements. The primary parameters include bearing outside diameter, inside diameter, raceway geometry, and cross-sectional dimensions.

Bearing Diameter and Height

The bearing’s outer diameter (OD) and inner diameter (ID) are determined by the available mounting space and the required clearance for bolts or welds. However, increasing the diameter also increases the lever arm for tilting loads, which can actually reduce load capacity per unit size. A larger bearing may be necessary for high tilting moments but may also increase weight and cost.

Raceway and Rolling Element Selection

Slewing bearings typically use ball or roller raceways. Four-point contact ball bearings are common for light to moderate loads and offer low friction. Crossed roller bearings provide higher rigidity and load capacity for heavy-duty applications. The choice affects not only load handling but also stiffness, rotational accuracy, and maintenance intervals. LYMC offers both types with optimized heat treatment and hardened raceways for extended service life.

Rotation Speed and Duty Cycle

While most slewing bearings operate at low rotational speeds (under 10 rpm), the duty cycle—number of oscillations or rotations over the equipment’s life—significantly influences bearing sizing. High-frequency oscillation can accelerate raceway wear, requiring a larger bearing or specialized lubrication system. For continuous rotation applications, consult the dynamic load rating and expected L10 life.

…

For more detailed information on selecting a slewing bearing to meet your equipment requirements, please click here: https://www.mcslewingbearings.com/a/news/slewing-bearing-sizing-guide.html

Crossed roller bearings are specified when a machine needs high rigidity, accurate rotation, and a compact envelope — robot joints, machine tool tables, indexing heads, and medical scanners all rely on them. Selecting the wrong configuration, precision grade, or mounting method can degrade positioning accuracy, shorten service life, and inflate cost. This guide explains the structure, the selection parameters that matter, the main design variants, and a step-by-step process engineers can follow to reach a defensible choice.

What Makes a Crossed Roller Bearing Different

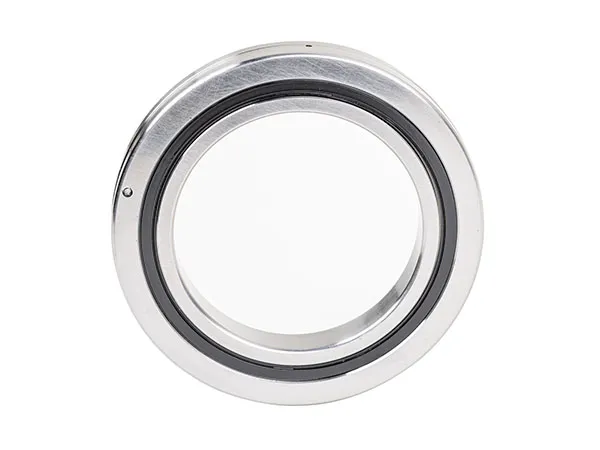
A crossed roller bearing has cylindrical rollers arranged at 90° to one another in a single raceway, alternating in sequence along the circumference. Because the rollers cross, one bearing set carries radial, axial, and moment loads simultaneously. That is the core reason designers choose it over a pair of angular contact ball bearings or a conventional thrust-plus-radial combination.

Structural Advantages

  • Single bearing replaces multiple load paths, reducing stack height and part count.
  • Line contact between roller and raceway produces high stiffness under load.
  • Alternating roller orientation limits elastic deformation to a predictable range.
  • Preloaded assemblies eliminate internal clearance and improve repeatability.

The trade-off is sensitivity to mounting accuracy and contamination. Crossed roller bearings reward careful design and punish shortcuts in housing preparation.

Key Parameters for Crossed Roller Bearing Selection

Crossed Roller Bearing

Selection is not a single calculation. It is a sequence of constraints that narrow the field from hundreds of catalog numbers to one or two viable options.

Load Capacity and Moment Rating

Every crossed roller bearing carries three load ratings: dynamic radial, dynamic axial, and moment. A robot arm joint may see a small axial force but a large tilting moment. A rotary table may see heavy axial load with modest moment. The selection process starts by resolving the actual load case — including shock factors and duty cycle — into these three components.

Never size a crossed roller bearing on radial load alone. Moment capacity frequently governs the final choice, especially in cantilevered or offset-load arrangements.

Precision Grade and Rotational Accuracy

Precision grades for crossed roller bearings are typically defined by running accuracy, axial runout, and radial runout. Common tiers map to:

  • Standard grade for general indexing and slow rotation.
  • High grade for machine tool positioning and metrology.
  • Ultra-precision grade for semiconductor equipment and optical stages.

Higher grades cost more and demand tighter mounting surfaces. Specifying ultra-precision on a frame that cannot hold flatness tolerance wastes money.

Envelope, Mounting, and Preload

Crossed roller bearings are available with or without inner and outer mounting holes, in open or sealed configurations, and with different preload classes. A bearing with integral mounting holes simplifies housing design and reduces assembly error. Sealed units retain grease and exclude debris but add drag torque — a factor in high-speed or low-torque applications.

Operating Environment

Temperature range, vacuum exposure, washdown chemicals, and vibration all influence material, lubrication, and sealing choices. Bearings destined for cleanroom use may require vacuum-compatible grease or dry-film lubrication. LYMC supplies crossed roller bearings in configurations matched to these environments, with documentation that supports the selection record.

…

For more information on crossed roller bearings, please click to access the complete selection guide: https://www.mcslewingbearings.com/a/news/crossed-roller-bearings-selection-guide.html

Crossed roller bearings sit at the heart of positioning accuracy in CNC machines. A single wrong specification can introduce runout, reduce rigidity, or shorten service life, and the resulting scrap rate often costs far more than the bearing itself. For engineers and purchasing teams, the real challenge is not finding a supplier, but matching bearing type, precision grade, and stiffness to a specific axis, spindle, or rotary table. This guide explains the selection factors that matter most, the trade-offs behind each choice, and how to verify a supplier before committing to volume orders.

Why Crossed Roller Bearings Are Preferred in CNC Structures

Unlike standard ball bearings, a crossed roller bearing arranges cylindrical rollers at 90 degrees to each other, alternating in a single raceway. This layout lets one bearing absorb radial, axial, and moment loads simultaneously, which simplifies the surrounding mechanical design considerably.

For CNC applications the practical benefits are direct:

  • Higher rigidity per unit volume, which reduces elastic deflection under cutting force
  • Compact cross-section, allowing thinner rotary tables and joint arms
  • Consistent torque across the rotation range, improving interpolation accuracy
  • Reduced part count, since separate thrust and radial bearings are no longer required

These characteristics make crossed roller bearings a common choice for rotary tables, indexing heads, robotic joints, tool changers, and the tilt axes of five-axis machines.

Identify the Application Before Comparing Specifications

Selection starts with the axis itself, not the catalogue. A high-speed spindle axis and a slow rotary table demand very different bearings, even when their bore sizes match.

Define the Load Profile

Estimate the combined radial, axial, and moment loads, then apply a safety factor that reflects shock and intermittent cutting. Thin-section bearings are sensitive to moment load, so an underestimated overturning moment is one of the most frequent causes of premature failure.

Define the Motion Profile

Continuous rotation, oscillating motion, and indexing with frequent starts and stops each stress the raceway differently. Oscillating axes tend to show false brinelling if lubrication is inadequate, while indexing axes place more demand on cage or separator durability.

Define the Precision Requirement

Match the bearing’s running accuracy to the machine’s positioning tolerance rather than simply buying the highest grade available. Overspecifying precision adds cost without improving the finished part.

Match Bearing Type to the Axis

Crossed roller bearings for CNC equipment generally fall into a few practical categories:

  • Separator-type (caged) bearings — rollers are kept apart by spacers, giving lower friction and better suitability for higher speeds.
  • Full-complement bearings — maximum roller count and highest load capacity, but limited speed and higher friction.
  • Open and sealed designs — sealed versions resist chips and coolant but run slightly warmer.
  • Inner-rotation and outer-rotation variants — the mounting direction should follow how the machine structure transmits load.

…

For more detailed information on how to select crossed roller bearings for CNC machine tools, please click here: https://www.mcslewingbearings.com/a/news/cnc-crossed-roller.html

Selecting the right tunnel formwork system is a critical decision that directly impacts project timelines, budget, and final quality. For civil engineering professionals evaluating forming solutions, the choice between one-piece (full-section) and segmental (incremental) tunnel formwork is often the first crossroads. Each system offers distinct advantages depending on tunnel length, cross-section geometry, site logistics, and production volume. This article provides a technical, unbiased comparison of the pros and cons of both methods, drawing on Gaofei’s extensive experience in delivering customized formwork solutions for tunneling projects worldwide. By understanding these differences, you can make an informed decision that balances speed, cost, and structural integrity.

Understanding the Core Differences Between One-Piece and Segmental Tunnel Formwork

Structural Design and Assembly

One-piece tunnel formwork consists of a single, rigid steel or aluminum form that matches the entire cross-section of the tunnel. It is typically assembled on-site and moved as a monolithic unit using hydraulic or mechanical systems. In contrast, segmental tunnel formwork divides the cross-section into multiple segments — often a base slab, two side walls, and a top arch — that are installed sequentially. Segments are lighter and easier to handle individually but require more joint connections and alignment adjustments.

Application Scenarios

One-piece systems are ideal for short to medium tunnels with consistent cross-sections, such as subway stations, pedestrian underpasses, or small road tunnels. Segmental formwork excels in long tunnels, variable geometries, or projects with tight access constraints, where transporting a full-section form would be impractical. Gaofei’s engineering team often recommends segmental systems for large-diameter tunnels or those requiring multiple curves and tapers.

Key Advantages of One-Piece Tunnel Formwork

tunnel formwork system
  • Faster cycle times: A single form can be stripped, moved, and reset in one operation, reducing labor and crane time. Typical cycle times for one-piece systems are 1–2 days per pour.
  • Superior concrete finish: Fewer joints mean less grouting and surface repair. The monolithic pour eliminates cold joints and alignment mismatches.
  • High dimensional accuracy: The rigid structure maintains strict tolerances, critical for tunnels with waterproofing membranes or precast lining integration.
  • Lower initial labor cost: Fewer components simplify assembly and require less skilled labor compared to segmental systems with multiple connection points.
  • Ideal for repetitive short runs: When the tunnel length is limited (e.g., 50–200 meters), the transport and handling challenges of a large form are manageable.

Key Advantages of Segmental Tunnel Formwork

  • Flexibility in geometry: Segments can be adjusted independently to accommodate varying cross-sections, curves, or tapers without building a completely new form.
  • Easier logistics and transport: Each segment fits standard shipping containers or trucks, reducing shipping costs and allowing use in remote or urban sites with limited crane capacity.
  • Reduced storage footprint: Segments can be stored on-site in a smaller area and assembled incrementally as the tunnel progresses.
  • Lower initial investment: Building a segmental form typically requires less steel and simpler fabrication, making it cost-effective for projects with uncertain or phased schedules.
  • Simpler maintenance and repairs: Damaged segments can be replaced individually without dismantling the entire system.
  • Adaptable to long tunnels: For tunnels exceeding 500 meters, segmental systems allow continuous casting while the form moves along the tunnel, avoiding the need to reposition a massive single piece.

For more detailed information on the pros and cons of monolithic versus segmental tunnel formwork, please click here: https://www.gf-bridge-tunnel.com/a/blog/tunnel-formwork-pros-cons.html

Specifying tunnel formwork for high-strength concrete demands a rigorous approach that goes beyond standard formwork selection. High-strength concrete—typically defined as concrete with compressive strength above 60 MPa—exhibits lower workability, higher density, and greater autogenous shrinkage, which impose unique stresses on formwork systems. The formwork must not only withstand higher hydrostatic pressures but also maintain strict dimensional tolerances and surface finish quality. For engineers and contractors, the specification process requires careful evaluation of load capacity, stiffness, joint tightness, and release agent compatibility. This article provides a structured guide to specifying tunnel formwork specifically for high-strength concrete, drawing on Gaofei’s long-standing experience in delivering robust formwork solutions for demanding infrastructure projects.

Understanding the Challenges of High-Strength Concrete in Tunnel Formwork

High-strength concrete behaves differently from conventional concrete during placement and curing. Its lower water-cement ratio results in higher viscosity and greater lateral pressure against formwork—especially during initial setting. Additionally, the reduced bleeding means less self-lubrication between concrete and form panels, increasing the risk of surface defects. These characteristics directly affect formwork specification:

  • Higher hydrostatic pressure: Lateral pressure can exceed 100 kN/m² for rapid pours. Formwork must be designed with a safety factor of at least 1.5 against overturning and bursting.
  • Reduced workability: Requires smoother form surfaces and effective vibrator access points to avoid honeycombing.
  • Increased shrinkage and cracking potential: Formwork restraint must be limited; careful joint design is needed to allow controlled movement during early curing.
  • Demanding surface quality: High-strength concrete magnifies surface imperfections—every blemish, joint mismatch, or stain becomes visible and structural.

Key Specification Parameters for Tunnel Formwork Systems

Tunnel Formwork

When drafting a technical specification for tunnel formwork intended for high-strength concrete, the following parameters must be clearly defined:

Load Capacity and Stiffness

The formwork must be rated to withstand the full lateral pressure of high-strength concrete without excessive deflection. Specify minimum design loads based on concrete density (typically 2500 kg/m³) and pour rate (up to 2 m per hour). Minimum stiffness: deflection limited to L/400 or 3 mm, whichever is stricter. For tunnel formwork, consider both internal and external loads—including equipment, crew, and wind if applicable.

Surface Finish and Panel Material

High-strength concrete requires form panels with very low porosity to prevent water absorption and staining. Recommend steel-faced panels (thickness ≥ 4 mm) or high-density overlaid plywood with sealed edges. Specify surface roughness (Ra ≤ 6.3 μm for visible concrete). Ensure all joints are flush, with no gaps exceeding 0.5 mm.

Sealing and Joint Tightness

Leakage at form joints causes sand runs and aggregate exposure—unacceptable for high-strength concrete. Require continuous gaskets at all panel connections and a positive locking mechanism. Provide a maximum grout leakage allowance of 0.1 L per linear meter of joint per hour under full hydrostatic pressure.

Release Agent Compatibility

High-strength concrete demands release agents that do not react with cement or leave residues that compromise bond-to-reinforcement. Specify oil-based or water-based release agents with proven performance on identical concrete mixes. Ban the use of diesel or low-quality oils that can cause discoloration.

…

For more details on how to specify tunnel formwork for high-strength concrete, please click here: https://www.gf-bridge-tunnel.com/a/blog/how-to-specify-tunnel-formwork-for-high-strength-concrete.html